Microbial Contamination in Coolant: How to Detect, Prevent and Treat It
Coolant (KSS) management concerns both machining quality and exposure to fluid and mist. Monitor microbial contamination alongside concentration, pH, tramp oil and system cleanliness. A normal appearance or lower particle load does not establish acceptable microbial counts.
Fluid-quality management also needs exposure controls, including skin-contact precautions, enclosures and mist ventilation as identified by the site risk assessment. See UK HSE guidance on metalworking-fluid health risks and controls; apply local requirements and competent site assessment.
A putrid or “rotten egg” smell often indicates increasing anaerobic decomposition.
Discolouration
Grey-black, brown or unusually cloudy fluid may be linked to microbial growth, sludge and decomposition products.
Foaming
A sudden increase in foam can indicate that microbial metabolites are disrupting the emulsion.
Trends
Track fluid-quality trends alongside direct microbial measurements; chemical readings alone do not establish microbial contamination.
02
Early Detection
Do not rely on odour alone: combine sensory checks with data trends
Odour and Appearance
Putrid or sour odours, obvious discolouration, increased sediment or emulsion separation all require further investigation. A normal smell does not necessarily mean that microbial counts are acceptable.
Foaming and Machining Performance
Abnormal foaming, reduced cooling performance, shorter tool life, workpiece corrosion or fluctuating surface quality may result from a combination of fluid chemistry and microbial activity.
On-Site and Laboratory Testing
Record concentration, pH, nitrite, hardness and temperature, and measure microbial contamination directly with dipslides or another suitable method. Chemical readings and appearance do not replace microbial testing. Use laboratory support when the result is unclear or organisms need to be identified.
pH
Watch for a sustained decline
NO₂⁻ / NO₃⁻
Compare trends with the initial value
Colonies and Appearance
Laboratory analysis when required
Chemical Trends Do Not Replace Microbial Testing
Nitrate and nitrite should be assessed with make-up-water quality and the coolant history; a nitrate increase alone does not establish bacterial or fungal contamination. Use direct microbial measurements alongside fluid-quality checks. UK HSE monitoring guidance describes weekly dipslide testing, with reduced frequency supported by effective-control records and the risk assessment. Follow the test supplier instructions for sampling, incubation and reading results. See the coolant testing guide for the other parameters.
03
Causes of Contamination
Temperature, nutrients, dead zones and tramp oil create ideal growth conditions
Microorganisms may enter through make-up water, workpieces, personnel, air or equipment surfaces. Tramp oil and some organic residues can add to contamination, while particles, sludge and equipment dead zones provide attachment and accumulation sites. Do not treat metal particles themselves as a universal microbial nutrient source. Investigate conditions using microbial trends, fluid condition and maintenance records.
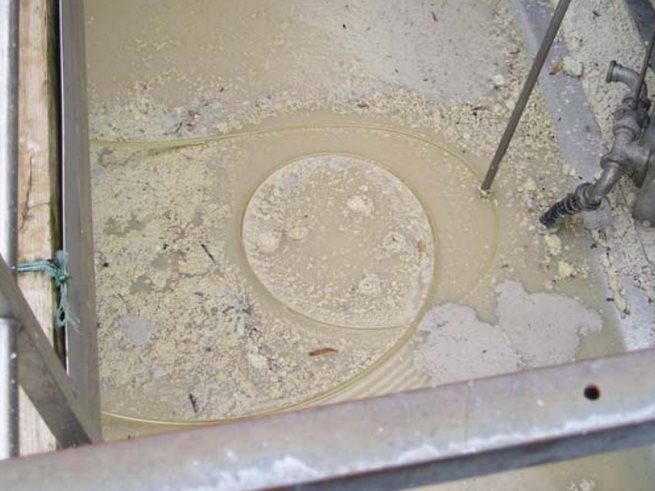
Tramp oil covering the surface:Restricts oxygen exchange and promotes anaerobic conditions below the surface.
Return-flow and pipe dead zones:Low flow encourages biofilm formation and repeated contamination of the main tank.
Uncontrolled concentration or pH:Weakens the formulation’s inherent stability and microbial resistance.
Continuous contaminant ingress:Slideway oil, hydraulic oil, fine metal particles and organic residues feed microbial populations.
Key Point
Disinfection can only reduce microbial counts temporarily. If tramp oil, particles, dead zones and concentration deviations remain, contamination is likely to return.
Continuous removal of tramp oil and particles, combined with effective circulation, reduces available nutrients and low-oxygen zones.
04
Prevention First
Use consistent routine maintenance to prevent rapid microbial growth
Control Make-Up Water and Concentration
Mix the fluid according to the supplier’s instructions, use suitable water quality and regularly verify concentration, pH and temperature. Avoid incorrect ratios and frequent unmeasured additions.
Inspect the liquid surface, odour and foam daily; measure concentration and pH on schedule; and regularly clean filters, tank bottoms and return-flow dead zones. Preventive maintenance usually costs less than treating an entire contaminated system.
05
Reducing Existing Microbial Counts
Thermal treatment and biocides each have specific limits
Thermal Treatment
A thermal process should be considered only after the coolant supplier or a qualified service provider has assessed formulation and equipment suitability. Temperature, holding time, mixing and uniformity must be validated together; reaching a single temperature does not establish sterilisation.
Check the effects on fluid performance, equipment and operator safety, and compare microbial results before and after treatment. Thermal treatment does not replace oil removal, filtration or system cleaning.
Drawbacks include relatively high energy demand, whose cost impact increases with treated volume. Equipment suitability, temperature uniformity and the formulation’s temperature tolerance must be assessed before implementation.
Validate time and temperature
No added biocide
Assess energy use
Biocides
Biocides can reduce microbial counts quickly, but the product must be compatible with the coolant formulation and used in strict accordance with dosage, occupational-safety and regulatory requirements. Under the CLP system, some products may be classified as hazardous; improper use can irritate skin, eyes and mucous membranes or cause allergic reactions.
Use only on professional advice
Avoid overdosing
Use appropriate PPE
Treatment Principle
Thermal treatment or biocides only reduce microbial counts; they do not replace tramp-oil removal, filtration, cleaning dead zones, or correcting concentration and pH deviations. The coolant supplier, occupational-safety personnel or a qualified service provider should select the method based on microbial counts, fluid condition and the root cause of contamination.
06
Severe Deterioration
Once the fluid has become unstable, complete fluid replacement is usually necessary
Severely deteriorated KSS often cannot be restored by disinfection alone. Microorganisms metabolise formulation components and alter the original composition until the fluid no longer provides the required performance. The fluid should then be completely replaced while the causes of bacterial or mould contamination are identified and eliminated.
Confirm the contamination level, fluid chemistry and likely sources.
Drain the old fluid correctly and dispose of it in accordance with local requirements.
Clean the tank, pipework, pumps, filters and low-flow dead zones.
Rinse thoroughly so that old fluid, biofilm and cleaner residues are not left behind.
Mix the replacement fluid in the correct sequence and resume scheduled monitoring records.
Address the Root Cause at the Same Time
Check the sources of tramp oil, return-flow design, surface coverage, shutdown duration, make-up water quality and concentration control. All equipment components must be thoroughly cleaned and rinsed before new KSS is added; otherwise contaminated residues can act as an inoculum and rapidly contaminate the fresh fluid.
07
Maintenance Conclusions
Move from reactive treatment to continuous control of contamination conditions
Continuous testing, documentation and maintenance of KSS are essential not only for workpiece quality, but also for the occupational health of metalworking personnel. If action begins only after odour or visible discolouration appears, the least costly intervention point has usually passed.
The choice of preventive filtration equipment depends on tank size, contaminant types and process requirements. An effective, sustainable solution should continuously remove tramp oil and particles while maintaining fluid mixing, oxygen exchange and stable operating parameters.
Compared with repeated emergency dosing, continuous control of contamination conditions is more effective in extending KSS service life, protecting employees and stabilising machining quality.
Evaluate the economics using site data for equipment and installation, consumables and energy, maintenance labour, fresh-fluid additions, waste disposal and downtime. Improved coolant management does not establish a short payback period for every equipment purchase.
A FRIESS EFR D8 electrostatic oil cleaner extended hydraulic-oil life from about two months to several years and reduced steel mill hydraulic failures by 70%.
After oil-bath hardening, a FRIESS Skimmtelligent 20 removes tramp oil from degreasing wash water so components can be cleaned reliably for downstream processing.
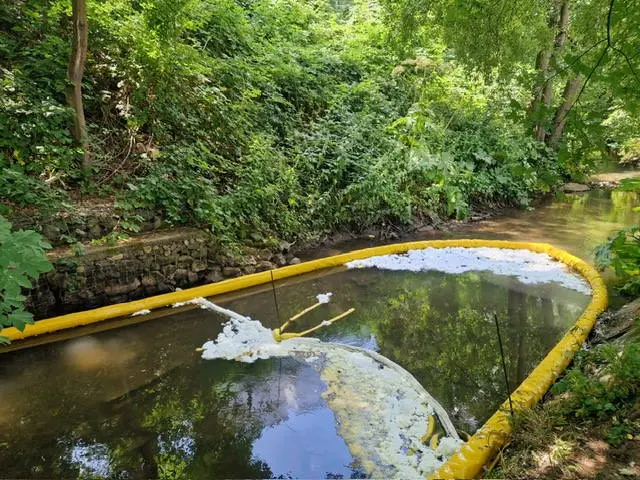
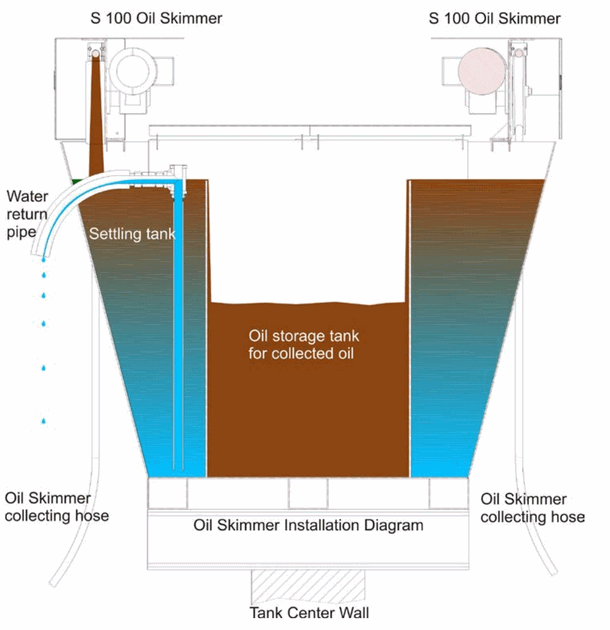
Transformer-oil spill case: a FRIESS S100 collected floating oil along a boom at a difficult-access stream site, helping contain further contamination.
Skimmtelligent Mini separates free tramp oil and coalescible droplets from coolant and wash water. Fluid care still requires condition and microbial monitoring.
A FRIESS S100 oil skimmer replaced a maintenance-intensive mop skimmer in a steel mill clarifier, cutting conversion costs below one year of previous repair expenses.
At a large metalworking plant with around 300 machine tools, a FRIESS 1U oil skimmer reduced coolant contamination, extended service life from weeks to one year and paid back in under six months.
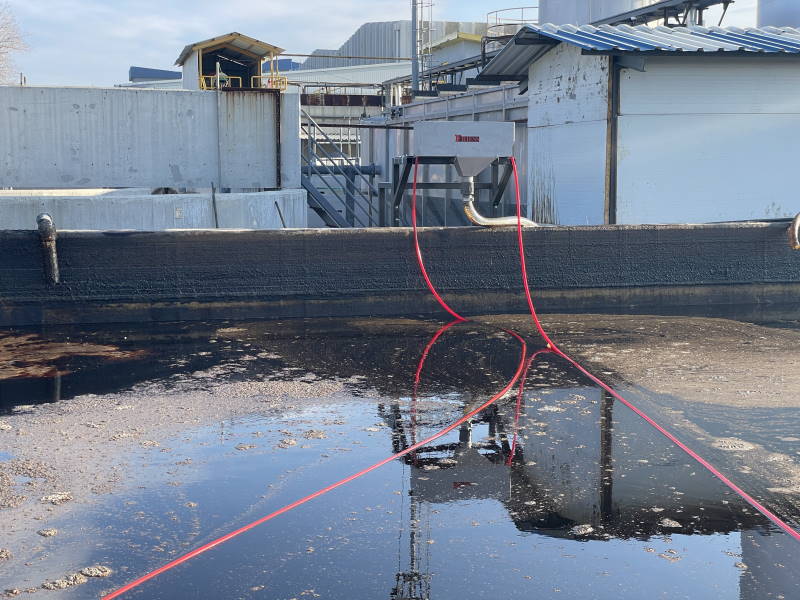
The FRIESS W40 collects tramp oil and floating oily sludge from the coolant surface in grey cast iron machining, reducing the black contamination layer and supporting subsequent coolant maintenance.
A practical guide to monitoring coolant concentration, pH, nitrite and microbial contamination so adverse trends can be corrected before odour, corrosion, tool wear or rejects occur.
FMF 420/6 grinding-coolant case: sample analysis found no detectable particles, surface quality improved, and no further grinding complaints were recorded.
A FRIESS W40 hose oil skimmer removes a thick floating fat layer from process wastewater at the Plukon Food Group, reducing odour, disposal costs and treatment disruption.
A FRIESS S100 tube oil skimmer removes floating hydrocarbons from parking lot wastewater as part of a two-stage process that achieves low HC concentrations.
A European gearbox plant used a FRIESS EFR D8 electrostatic oil cleaner to reduce hydraulic-oil particles larger than 4 µm by about 90% in a 23-hour test.
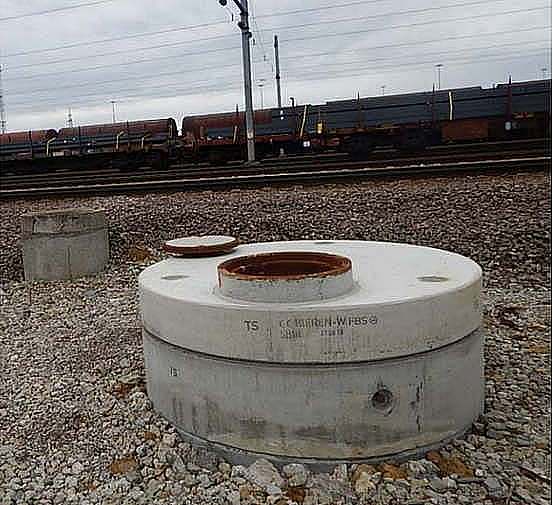
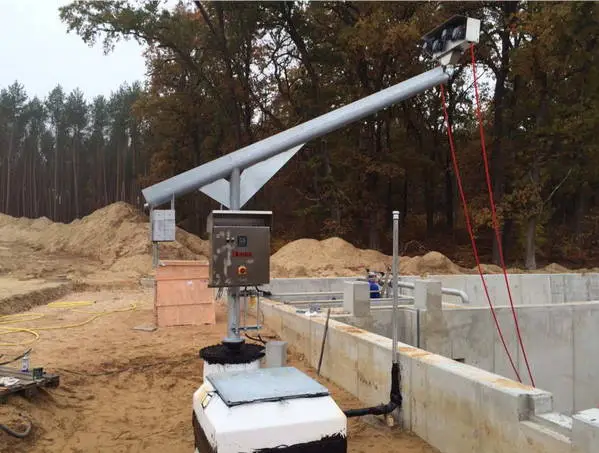
A FRIESS tube oil skimmer continuously removes leaked hydraulic oil from a rail yard’s surface drainage system, protecting a nearby river during heavy rain.
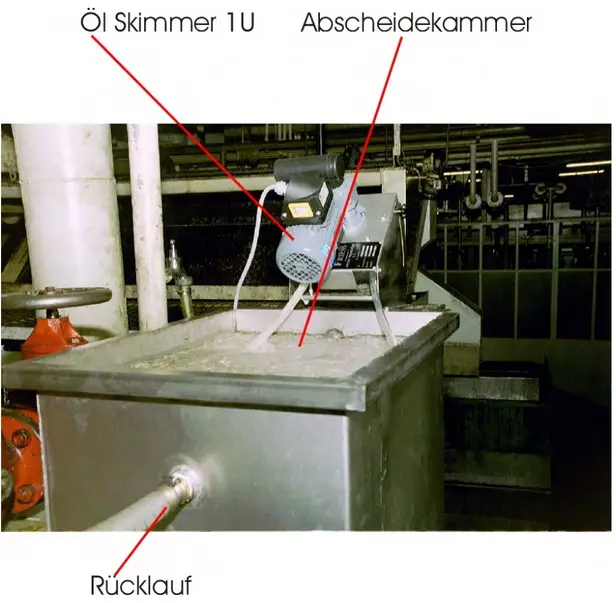
A FRIESS 1U oil skimmer with an extended collection tube removes tramp oil across a large machining-centre coolant tank, extending coolant service life.
A FRIESS W40 oil skimmer removed oil and grease from a steel mill cooling-water clarifier, protecting the downstream gravel filter for more than three years.
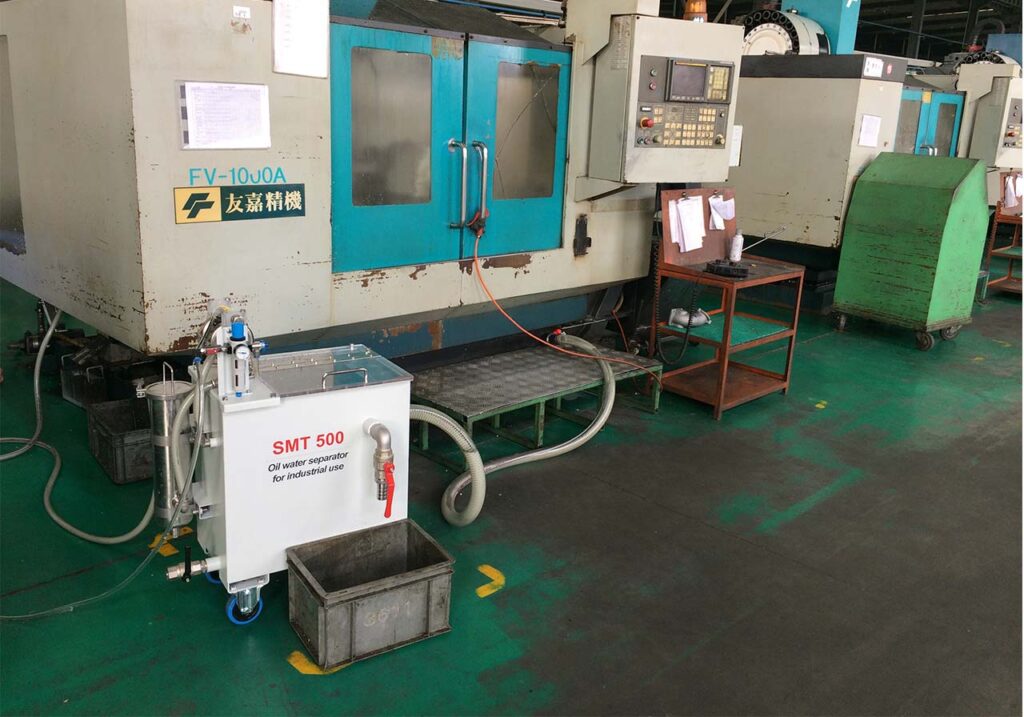
The FRIESS SMT500C uses mobile bypass circulation to remove tramp oil and suspended particles from machining-centre coolant sumps, improving fluid stability and reducing maintenance.
A FRIESS EFC D4 electrostatic oil cleaner removed fine particles and oxidation products from hydraulic test-bench oil, visibly improving cleanliness within two weeks.
A FRIESS Skimmtelligent oil separator keeps tramp oil below 50 L in a 30 m³ central coolant system, extends emulsion life to one year and pays back in under six months.
Particle contamination causes wear and can impair hydraulic components. This guide explains oil analysis and electrostatic cleaning, with performance assessed for the oil and operating conditions.
FRIESS S100 oil skimmers remove floating oil from tank wash water at three German Armed Forces sites using custom swivel booms, collection tanks and remote monitoring.
Four FRIESS EFR D16 electrostatic oil cleaners treated 120,000 litres of HLP 46 hydraulic oil, removed oxidation products and reduced the MPC value from 60 to 8.
In this injection-moulding case, EFR D8 cleaning reduced hydraulic failures and filter consumption. No oil changes were reported during follow-up; future replacement still depends on oil analysis.
FRIESS Skimmtelligent continuously removes oil from a degreasing bath, reducing chemical consumption, stabilising the process and protecting coating quality.
Learn how ISO 4406 particle counts, wear metals, viscosity, TAN and PQ index reveal hydraulic oil contamination, filtration performance and maintenance needs.
An 11-year-old injection moulding machine failed every two weeks; FRIESS EFR D8 removed sludge, fine particles and oxidation products, reducing failures to zero.
In this cast-iron machining case, FMF 310/3 removed fine iron particles while site records showed low coolant bacteria. Magnetic filtration is not a disinfection process.
A FRIESS S100 oil skimmer automatically removes floating fat from food-industry process wastewater before treatment, reducing the load on downstream separation and treatment processes.
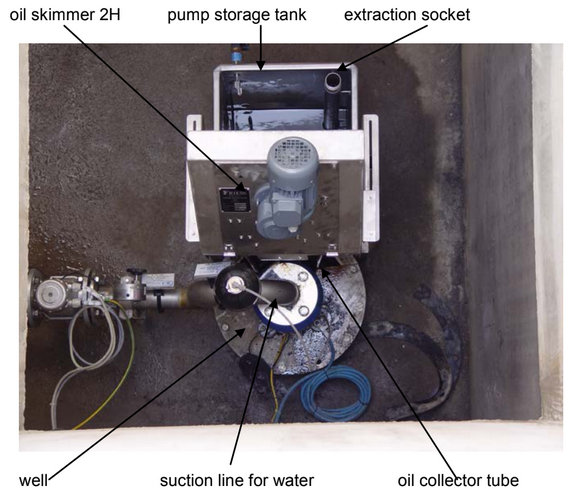
A FRIESS Model 2H tube oil skimmer removes hydrocarbon contamination from refinery groundwater wells and, after initial cleanup, needs only about five minutes of operation per week.
A FRIESS S100 oil skimmer removes floating oil from steel mill cooling-water clarifiers, reducing hydrocarbon carryover and the load on downstream gravel filters.
A FRIESS W20 oil skimmer removes viscous oil, grease and release-agent residues from air scrubber wash water while preventing blockages and eliminating manual cleaning.
A FRIESS EFR D16 with automatic particle monitoring reduced hydraulic faults on four automotive presses by more than 80%, with payback in under six months.
A W40 skimmer collects floating oil and graphite-containing residues from automotive forging wastewater as a pretreatment step before downstream treatment.